
ASTM F136 bar is Ti-6Al-4V ELI for surgical implants. It differs from Grade 5 by tighter interstitials: oxygen 0.13% maximum against 0.20%, iron 0.25% against 0.30%. Bar is normally supplied annealed and centreless ground, commonly Ra 0.8 µm or better with a diameter tolerance around ±0.0127 mm.
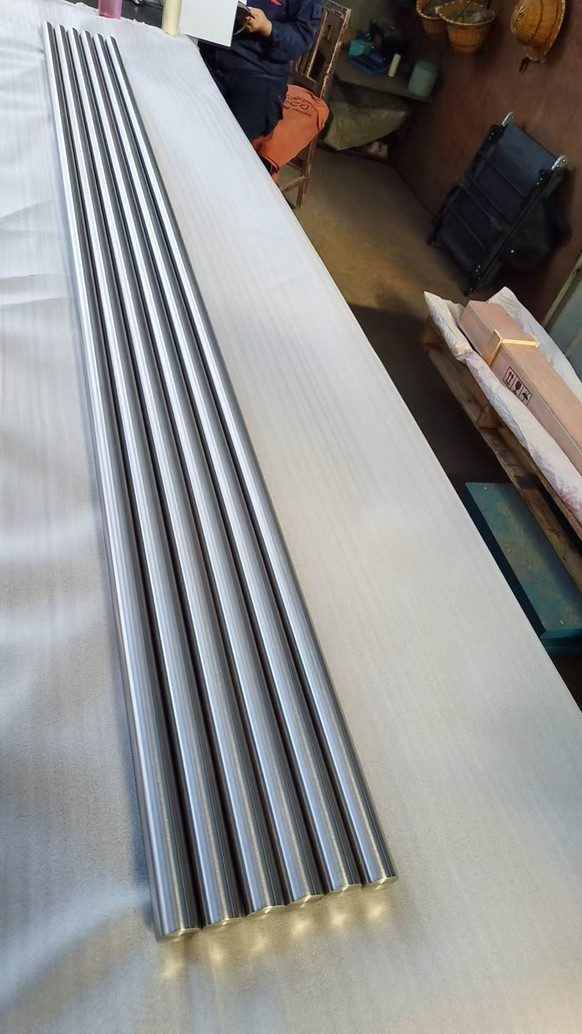
When a medical drawing calls for Ti-6Al-4V ELI to ASTM F136, the buyer is asking for more than standard Grade 5 with a different label. ELI chemistry, interstitial limits, and surface condition all change what the mill must control and what the certificate must show. This guide explains what F136 actually requires, how it differs from F1472 and commercial Grade 5, and how to put an F136 bar or wire RFQ together so it can be quoted without a second round of questions.
Beiyu Titanium supplies Ti-6Al-4V ELI bar to ASTM F136, precision centerless ground, alongside CP titanium bar to ASTM F67. When EN 10204 3.1 documentation and heat or lot traceability are required, state the reporting scope in the RFQ so it can be confirmed before order release.
For the wider qualification context, use Beiyu’s medical titanium materials overview; for a buyer-side comparison of implant grades, see the ASTM F67 vs F136 medical titanium guide.
This F136 guide is part of Beiyu’s titanium for medical implants hub, where F136 ELI is compared with F67, F1472 and the separate ISO 5832 material system.
What does ELI mean, and how is F136 different from standard Grade 5?
ASTM F136 covers wrought Ti-6Al-4V ELI, extra-low-interstitial alloy for surgical implant applications, UNS R56401. The base chemistry is the same 6% aluminium, 4% vanadium as standard Grade 5; what changes is the ceiling on interstitial elements:
| Parameter | Ti-6Al-4V ELI (F136) | Standard Ti-6Al-4V (Grade 5) |
|---|---|---|
| UNS number | R56401 | R56400 |
| Oxygen, max | 0.13% | 0.20% |
| Nitrogen, max | 0.05% | 0.05% |
| Carbon, max | 0.08% | 0.08% |
| Hydrogen, max (bar) | 0.012% | 0.015% |
| Iron, max | 0.25% | 0.40% |
| Character | Higher ductility and fracture toughness | Higher strength on paper |
Verify exact limits against the current revision of each standard; the certificate chemistry decides ELI status.
Lower interstitials trade a little strength for what implants actually need: higher ductility, better fracture toughness, and improved damage tolerance in the body. That is why load-bearing orthopedic, spinal and trauma implants are machined from ELI rather than standard Grade 5.
F136 or F1472: which specification does your drawing need?
Both are implant specifications for Ti-6Al-4V, and buyers see both on medical drawings.
| Specification | Grade | UNS on the certificate | What you are buying |
|---|---|---|---|
| ASTM F136 | Ti-6Al-4V ELI | R56401 | Extra-low interstitial: lower strength ceiling, higher fracture toughness |
| ASTM F1472 | Standard-interstitial Ti-6Al-4V | R56400 | Stronger on paper, with less fracture-toughness margin |
The drawing controls the choice; the two are not interchangeable and the UNS number on the certificate must match. ASTM F136 itself covers wrought ELI bar. If a drawing separately calls for another product standard, the purchaser and supplier must reconcile the grade designation and every chemical, mechanical and dimensional requirement rather than assume automatic dual certification.
For standard-interstitial Ti-6Al-4V outside the implant ELI lane, Beiyu’s AMS 4928 titanium bar guide explains the aerospace and performance bar specification and how it differs from ASTM B348 Grade 5.
If the drawing shifts from ELI bar to standard-interstitial implant Ti-6Al-4V or to implant forgings, our ASTM F1472 and F620 guide explains when the paperwork chain stays at R56400, when it stays at R56401, and when an industrial B381 forging moves to R56407 instead.
How should you specify F136 ELI bar for machining?
The RFQ items mirror precision CP bar, with ELI-specific additions. A complete ELI bar line looks like this:
| RFQ item | Typical medical call-out | Why it matters |
|---|---|---|
| Diameter tolerance | ±0.0005 in (±0.0127 mm); unilateral +0/-0.0004 in on Swiss stock | Feeds automatics without a cleanup pass |
| Surface finish | 32 RMS (≈0.8 µm) ground | Incoming inspection criterion |
| Condition | Annealed | Machinability and property baseline |
| Tensile / yield, min | ~125 / 115 ksi (860 / 795 MPa) annealed | Confirm against current F136 revision |
| Hydrogen | Standard 0.012% max; some drawings cap far tighter | Verified at the mill, not at goods-in |
| Standards cited | ASTM F136 | F136 covers wrought ELI bar; add another product standard only when the drawing separately requires it and all grade requirements are reconciled |
Line-by-line notes:
- Diameter and tolerance. Implant machining commonly specifies ±0.0005 in (±0.0127 mm), and unilateral tolerances such as +0/-0.0004 in appear on Swiss-lathe stock. Beiyu holds ±0.0005 in (±0.0127 mm) on centerless ground bar, reviewed per diameter before quoting.
- Surface finish. 32 RMS (≈0.8 µm) or better is the common ground-bar call-out.
- Condition. State the required condition; annealed is typical for machining stock.
- Mechanical minimums. Annealed ELI bar is commonly ordered against minimums in the range of 125 ksi tensile / 115 ksi yield (about 860 / 795 MPa); confirm exact values against the current F136 revision and the drawing.
- Interstitial limits. Some medical drawings cap hydrogen tighter than the standard itself. State any tighter-than-standard limit explicitly, because it must be verified at the mill, not at incoming inspection.
When a drawing calls out grain size together with hydrogen, use Beiyu’s separate guide to grain size and hydrogen control on medical titanium bar to prepare the RFQ and certificate checklist.
Does ASTM F136 cover wire as well as bar?
Yes. F136 covers bar, wire, forgings and other wrought forms, and implant programs regularly buy fine ELI wire on spools alongside ground bar, down to sub-millimetre diameters for device components. Beiyu supplies F136 ELI wire as well as bar, including fine diameters on spools, with each wire line reviewed per the customer’s diameter, tolerance and spool requirement. Specify diameter and tolerance, spool or cut length, and surface condition on the wire line the same way as for bar.
When is CP titanium to F67 the better choice?
Not every medical part needs alloy strength. Commercially pure titanium to ASTM F67 (Grades 1-4) offers maximum corrosion resistance, formability and proven bone contact behavior at lower strength, and is specified for many non-load-bearing device components. Beiyu supplies both: CP bar to F67 and ELI bar to F136, so mixed programs can source both grades against one supplier with one documentation chain. See our companion guide to specifying ASTM F67 medical-grade CP bar. For a broader procurement view of Grade 1-4 choices, use the CP grade selection guide.
What should the certificate package show?
For ELI material the paper trail carries extra weight, because ELI status is provable only by chemistry.
| Item in the package | What it must show |
|---|---|
| Melt route | Vacuum-melted material; the route is traceable through the heat number |
| EN 10204 3.1 mill test certificate | Full chemistry including the interstitials O, N, C, H and Fe, reported against the ELI limits |
| UNS designation | R56401 identified on the certificate, matching the F136 call-out |
| Heat number | Traceability back to the melt |
| Mechanical results | For the supplied condition and the supplied diameter |
How to read the F136 ELI certificate when it arrives
The entire difference between F136 ELI and standard Grade 5 lives in the interstitial columns of the certificate, so that is where acceptance is decided. Work down the certificate line by line against this table.
| Line on the certificate | ASTM F136 ELI | Standard Grade 5 | Acceptance rule |
|---|---|---|---|
| Oxygen | 0.13 percent max | 0.20 percent max | Above the ELI limit, the heat is not ELI |
| Iron | 0.25 percent max | 0.40 percent max | Above the ELI limit, the heat is not ELI |
| Hydrogen | 0.012 percent max | 0.015 percent max | Above the ELI limit, the heat is not ELI |
| Nitrogen | Same limit for both grades | Not a discriminator between ELI and standard | |
| Carbon | Same limit for both grades | Not a discriminator between ELI and standard | |
| Tensile strength | 860 MPa min | 895 MPa min | Accept against the F136 minimum, not the Grade 5 one |
| Yield strength | 795 MPa min | 828 MPa min | Accept against the F136 minimum |
| Elongation | 10 percent floor for both | A healthy ELI heat shows its margin here and in reduction of area | |
| Melt route | Vacuum melted, traceable through the heat number | Confirm the certificate ties to a vacuum-melted heat | |
| Heat number | Printed on the certificate | Match it to the marking on the bar or spool | |
| Drawing-specific hydrogen cap | Only if you ordered one | Verify at the mill; it cannot be established at incoming inspection | |
ELI trades a little strength for higher ductility and fracture toughness, which is why the F136 minimums sit below Grade 5 while the elongation floor stays the same. The trap is a certificate that says Ti-6Al-4V or Grade 5 without ELI interstitial results. That is not F136, whatever the title says, because the qualification is entirely in the interstitial numbers.
For medical scope, material can be sourced from mills operating certified ISO 13485 systems, and the producing mill’s quality certificates accompany the material per order, so the certificate entity always matches the mill on the MTC.
Common medical bar diameters are available as standard; less common sizes are reviewed per the customer’s requirement before quoting rather than quoted from a fixed list.
When the order moves from wrought bar or wire into implant forgings, our ASTM F620 forging spec guide explains how the forging keeps the UNS of the source material specification.
The microstructure clause: what F136 requires beyond chemistry
ASTM F136 is not only a chemistry and tensile specification. It carries microstructure acceptance requirements, because implant performance depends on structure as well as composition.
| What F136 works to | Why | |
|---|---|---|
| Accepted | Primary alpha, equiaxed or elongated, in a transformed beta matrix, processed in the alpha-beta field | The structure the specification is written around |
| Excluded | A continuous alpha network along prior beta grain boundaries | A fatigue rule written as metallurgy: continuous grain-boundary alpha gives a crack an easier path |
| What the buyer writes | Microstructure acceptance per F136 applies, and the mill confirms it in the documentation package | Structure is set by thermomechanical processing at the mill and cannot be corrected downstream by heat treatment alone |
How grain size is measured and how hydrogen is controlled alongside it are covered in the grain size and hydrogen control guide.
Why ELI: the fatigue and damage-tolerance logic
The reason a hip stem or bone screw is machined from ELI rather than standard Grade 5 is not the tensile table, where standard Grade 5 actually wins.
| What the ELI trade gives up | What it buys | Why that is the right trade for an implant |
|---|---|---|
| Peak strength: F136 minimums sit below standard Grade 5 | Higher fracture toughness and ductility from lower oxygen and iron | Damage tolerance: the ability to live with the small flaw, scratch or inclusion that real manufacturing and real service eventually produce |
| Nothing on the chemistry that a buyer sees as a benefit | Tolerance of imperfection under cyclic load | An implant is cyclically loaded inside a body, where inspection and replacement are surgery |
| Attention that would go to the strength row | Attention on the surface and microstructure rows | Titanium fatigue is dominated by the surface: machining marks, embedded contamination and handling damage usually cost more fatigue life than the gap between two nearby strength grades adds |
That is why the surface and microstructure lines on an F136 order deserve the same attention as the chemistry table, and why the ELI trade, a little strength for a lot of tolerance, remains the default choice for structural implants.
Machining ELI bar: surface integrity is the deliverable
Implant shops machine F136 bar into screws, pins and stems where the machined surface becomes the fatigue-critical surface of the finished device. Ti-6Al-4V ELI follows the usual titanium rules: low speed, steady feed, rigid setup and generous coolant. It adds a medical-chain discipline: finishing passes should cut cleanly rather than rub, because a rubbed or smeared surface carries exactly the damage that cyclic loading finds first. Plan machining allowance so the finished surface sits in clean parent metal, and treat deburring and edge finishing as fatigue operations rather than cosmetics. The general machining behaviour of the alloy, including why it galls and work-hardens at the tool, is covered in the Ti-6Al-4V galling and work-hardening guide. For implant programs, surface integrity is not a workshop preference. It is part of the product definition.
Handling and identity: protecting the audit trail
Medical-chain bar carries two things that must survive storage and transport: a clean surface and a provable identity.
| Handling rule | What goes wrong without it |
|---|---|
| Keep titanium separated from carbon-steel racks and tools | Embedded iron particles stain, can seed localised attack, and fail surface-iron checks on certified work |
| Keep lots separated by heat | Heats mix, and the lot can no longer be tied to one certificate |
| Keep the heat-number marking legible until the last bar is used | An unmarked offcut cannot be traced, whatever alloy it is |
| Keep the certificate travelling with the material | A bar that cannot be tied to its heat has lost its implant-chain identity |
The full buyer-side ordering discipline, from the specification line to the packing line, is in the medical titanium bar RFQ checklist.
Limitations: what F136 ELI does not promise
| What F136 ELI does not promise | Why | Where the answer sits |
|---|---|---|
| It is not the strongest Ti-6Al-4V | Standard-interstitial Grade 5 and ASTM F1472 carry higher strength ceilings; ELI deliberately gives some of that away | Where the drawing calls F1472, supply F1472. See the ASTM F1472 and F620 guide |
| It qualifies material, not devices | F136 bar is implant-grade input stock | Biocompatibility, design and approval of the finished device belong to the device maker’s file, not the mill certificate |
| It does not protect against downstream hydrogen pickup | Aggressive pickling or poorly controlled chemical cleaning after delivery can load hydrogen into the surface and embrittle it | The certificate limit protects the delivered state, not what happens after |
| It does not stop titanium-on-titanium galling | Bone screws driven against titanium plates, and any sliding titanium interface, will gall | The design side: lubrication, coating or geometry. The alloy will not provide it alone |
Frequently asked questions
Is ASTM F136 the same as Grade 23 titanium?
Effectively yes for implant work: Grade 23 is the common name for Ti-6Al-4V ELI, and ASTM F136 is the surgical-implant specification for that alloy, UNS R56401.
What is the difference between ASTM F136 and ASTM F1472?
F136 is Ti-6Al-4V ELI (R56401) with tighter interstitial limits for fracture toughness; F1472 is standard-interstitial Ti-6Al-4V (R56400) for implants. The drawing decides which applies.
Can F136 bar be supplied precision centerless ground?
Yes. Implant machining stock is routinely supplied centerless ground to a stated diameter tolerance and surface finish, commonly ±0.0005 in and 32 RMS.
How do I verify material is really ELI?
By the certificate: chemistry must meet the ELI interstitial limits and the UNS number must read R56401. A bar certified only to standard Grade 5 (R56400) is not F136 material.
References
- ASTM F136, Standard Specification for Wrought Ti-6Al-4V ELI Alloy for Surgical Implant Applications: astm.org/f0136
- ASTM F1472, Standard Specification for Wrought Ti-6Al-4V Alloy for Surgical Implant Applications: astm.org/f1472
- ISO 5832-3, Implants for surgery, metallic materials, wrought titanium 6-aluminium 4-vanadium alloy. This ISO implant standard covers standard-interstitial Ti-6Al-4V and is not an ELI specification: iso.org/standard/79689
- EN 10204, Metallic products, types of inspection documents (CEN)
The melt route behind an ELI heat, and why the count matters
Interstitial limits are only half of what makes ELI material behave; the other half is how clean the melt is. The specifications that fix a melt route set a modest floor: AMS 4911 calls for first melt by vacuum consumable electrode, which is a single vacuum melt. Two heats can both meet the F136 chemistry and mechanical tables while carrying very different inclusion populations, because cleanliness follows the melt route rather than the composition limits.
Beiyu Titanium melts implant-chain material three times under vacuum before it becomes bar. Each remelt refines the structure and reduces the inclusion and segregation risk that fatigue-critical implant work is sensitive to, which is why a third melt is bought for cleanliness rather than for compliance. Beiyu ties the route to the heat number on the EN 10204 3.1 certificate, so the melt count is checkable against the material received rather than taken from a datasheet, and ultrasonic inspection is standard on the bar that comes out of it.
What an independent laboratory measured on an ELI lot against F136
ASTM F136 publishes limits. It does not tell a buyer how much room a real bar leaves against them, and that margin is one of the things a device manufacturer checks on receipt. The figures below are from one annealed Grade 23 bar lot supplied through the Beiyu implant chain and tested by an independent titanium testing laboratory.
| Property | Measured on the documented lot | ASTM F136 requirement | Test method |
|---|---|---|---|
| Hydrogen | 0.0014 % | ≤0.012 % | ASTM E1447-22 |
| Tensile strength Rm | 942 MPa | ≥860 MPa | ASTM E8/E8M-25 |
| Yield strength Rp0.2 | 882 MPa | ≥795 MPa | ASTM E8/E8M-25 |
| Elongation A4D | 19.0 % | ≥10 % | ASTM E8/E8M-25 |
| Reduction of area Z | 52 % | ≥25 % | ASTM E8/E8M-25 |
| Microstructure | Classified A3: equiaxed alpha in transformed beta, with no continuous alpha at the prior beta grain boundaries | Additional assessment, not an ASTM F136 requirement | ISO 20160:2006 Annex A and SAE AMS 2643F |
The hydrogen line is the one to read twice. At 0.0014 percent the lot used about a tenth of the F136 ceiling. Hydrogen is controlled on implant stock because excess hydrogen can promote hydride formation and embrittlement, and it is a chemistry limit rather than a strength metric. Elongation and reduction of area both came in at roughly twice their minima, which is ductility reserve rather than a compliance margin.
The microstructure classification is worth putting on the order explicitly. Class A3 under ISO 20160 Annex A describes equiaxed alpha within a transformed beta matrix with no continuous alpha network at the prior beta grain boundaries. A continuous alpha network at those boundaries is the feature the classification exists to identify. Note that this class is an ISO 20160 assessment, not a requirement written into ASTM F136 itself, so if the class matters to the application it has to be named on the order rather than assumed to come with the F136 callout.
Read these as results from documented production material, not as typical values and not as a level every heat will repeat. They show what the route produced on the material that was tested. Ask at enquiry which supporting records are available for the material being quoted, since the document scope and any redaction are agreed case by case rather than published here.
Specification detail with sources
ASTM F136 caps interstitial content well below standard Grade 5 limits: oxygen is held to 0.13 wt% max and iron to 0.25 wt% max (ASTM F136, Table 1), while Ti-6Al-4V bar supplied to ASTM B348 may run oxygen up to 0.20 wt%. Those lower limits are what the ELI designation actually buys for implant stock.
The UNS designation on the certificate should follow the standard on the order: material certified to ASTM F136 is designated UNS R56401, while Grade 23 bar certified to the ASTM B series (B348 for bar, B265 for plate) is designated UNS R56407. If the MTC shows one number and the purchase order names the other standard, query it before acceptance.
Request a quote for ASTM F136 ELI bar or wire
Use the titanium bar RFQ checklist to confirm that form, diameter, tolerance, condition, quantity and certificate requirements are complete before submission.
To quote implant-grade ELI material, Beiyu needs: form (bar or wire), diameter and tolerance, length or spool, surface finish, condition, mechanical minimums, and any tighter-than-standard interstitial limits. Send the drawing or spec and we review each line against grind and metallurgical capability before quoting, with EN 10204 3.1 MTC and heat-number traceability by order scope. Contact Beiyu Titanium for an RFQ.
Related Beiyu resources
- ASTM F67 Titanium Bar: Medical-Grade CP Bar for Machining
- ASTM B348 Titanium Bar & Billet Guide
- Titanium Materials for Medical Industry
- Medical-Grade Titanium: ASTM F136, F67 and Grade 23 ELI Explained
Reference sources
- ASTM F136, Standard Specification for Wrought Titanium-6Aluminum-4Vanadium ELI (Extra Low Interstitial) Alloy for Surgical Implant Applications (UNS R56401)
- ASTM B348 / B348M, Standard Specification for Titanium and Titanium Alloy Bars and Billets
- ASTM E112, Standard Test Methods for Determining Average Grain Size
- ISO 5832-3, Implants for surgery, Metallic materials, Part 3: Wrought titanium 6-aluminium 4-vanadium alloy
- EN 10204, Metallic Products, Types of Inspection Documents